In sheet metal bending and forming, warping, localized distortion, and corner tearing are common manufacturing defects. These issues typically stem from insufficient material support in the bend zone, cutouts positioned too close to the bend line, and stress concentration at corners. By optimizing flange length, cutout positioning, and bend relief structures during the design stage, you can eliminate the risk of bending deformation at the source and achieve consistent precision and structural integrity.
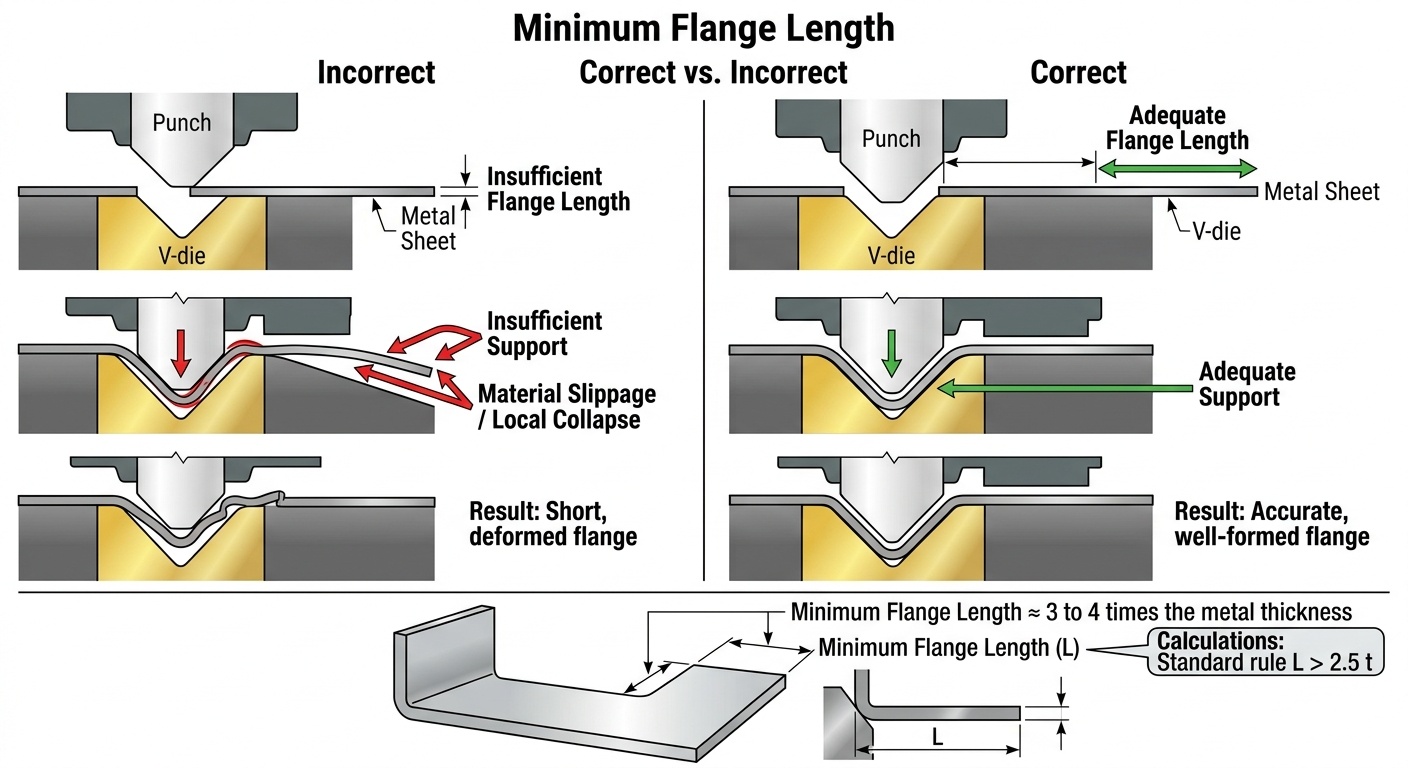
Sheet metal bending relies on upper and lower tooling to apply forming forces, which requires flanges on both sides of the bend line to have sufficient length to form a continuous, stable load-bearing surface. Insufficient flange length prevents the sheet metal from receiving adequate die support, leading to material slipping, stretching, or localized collapse during bending.
Different material thicknesses impose distinct requirements on minimum flange length and support coverage across the total bend length:
Thicker materials require higher forming forces, making continuous flange support even more critical. If support length is insufficient, thick plates are prone to material shift, over-stretching, and out-of-tolerance bend angles.
Placing holes, notches, edge cutouts, or other feature cuts too close to the bend line causes severe feature distortion due to plastic material flow during sheet metal bending. This also weakens structural strength within the bend zone, further magnifying bending deformation risks.
For standard air bending processes, cutouts should generally maintain a safety distance of at least 1/2 of the lower V-die opening width from the bend line to keep features outside the primary tooling engagement zone. Specific clearance requirements should be verified based on material type, sheet thickness, and actual tooling parameters. Designers can use manufacturing simulation software to flag high-risk deformation zones and validate feature placement.
In addition to safety distance, you must limit the total percentage of cutouts within the bend warning zone to maintain adequate material support:
When a bend meets a part corner or when adjacent bends are spaced too closely, the material at the corner experiences multi-axial stress concentration. This frequently results in severe wrinkling, material bulging, or corner tearing.
Standard DFM for sheet metal provides two effective solutions for these scenarios:
Formability varies significantly across material grades; standard design parameters cannot be universally applied without adjustments.
Review these essential checklist items prior to submitting your design for manufacturing:
Preventing bending deformation fundamentally relies on matching part design to the physical forces of the sheet metal bending process. Following robust DFM for sheet metal principles guarantees continuous material support and structural strength throughout the forming zone. Compliant designs prevent cosmetic and structural defects, improve dimensional consistency, and significantly cut prototyping rework costs.