Designing a rigid-flex PCB layout requires a fundamentally different approach than standard rigid boards. The combination of rigid FR4 sections and flexible polyimide (PI) regions introduces unique mechanical, thermal, and electrical challenges that every PCB layout engineer must address. This comprehensive guide covers material selection, bend area routing, via design, impedance control, and manufacturing considerations to help you create robust rigid-flex PCB layouts that survive thousands of flex cycles.
The flexible section of a rigid-flex PCB should always use polyimide (PI) instead of FR4. For applications involving repeated bending, use thinner PI films (12.5 μm or 25 μm). Slightly thicker PI can be used for static flex sections. Polyimide offers excellent heat resistance and flexural durability, while conventional FR4 is rigid and prone to cracking under repeated bending.
The PCB stackup should be planned independently for the rigid and flexible regions. Select prepreg (PP) materials separately for the FR4 rigid section and the PI flexible section. Mixing prepreg materials is not recommended because the large difference in the coefficient of thermal expansion (CTE) between FR4 and PI can cause warpage, delamination, and lamination defects.
For dynamic bending applications, always use Rolled Annealed (RA) copper foil instead of standard electrodeposited (ED) copper. RA copper provides superior ductility and significantly improves resistance to copper fatigue and cracking. ED copper is generally acceptable for static flex applications, but RA copper is still preferred for better reliability.
Avoid abrupt layer-count changes between rigid and flexible sections. Instead, use a gradual step-down stackup transition to distribute lamination stress more evenly and reduce the risk of delamination at the rigid-flex transition.
Large components such as BGAs, QFNs, connectors, transformers, and other heavy devices should always be mounted on the rigid section. Do not place SMT or through-hole components in flexible areas, as repeated bending can concentrate mechanical stress and lead to solder joint fatigue or failure.
Avoid routing traces or placing vias directly on the bend centerline (neutral axis). Whenever possible, route traces close to the neutral layer, where bending stress is minimized, greatly improving copper reliability.
Do not place plated vias, tooling holes, large pads, or solid copper pours within bending regions. These features create stress concentration points that can initiate cracks after repeated flexing.
Copper traces within the bending area should always run perpendicular to the bend axis. Traces routed parallel to the bend direction experience significantly higher tensile and compressive stress, increasing the likelihood of copper fracture.
Parallel traces in the flex region should maintain consistent width and spacing. Avoid mixing narrow and wide traces within the same bending area because uneven stress distribution often causes thinner traces to fail first.
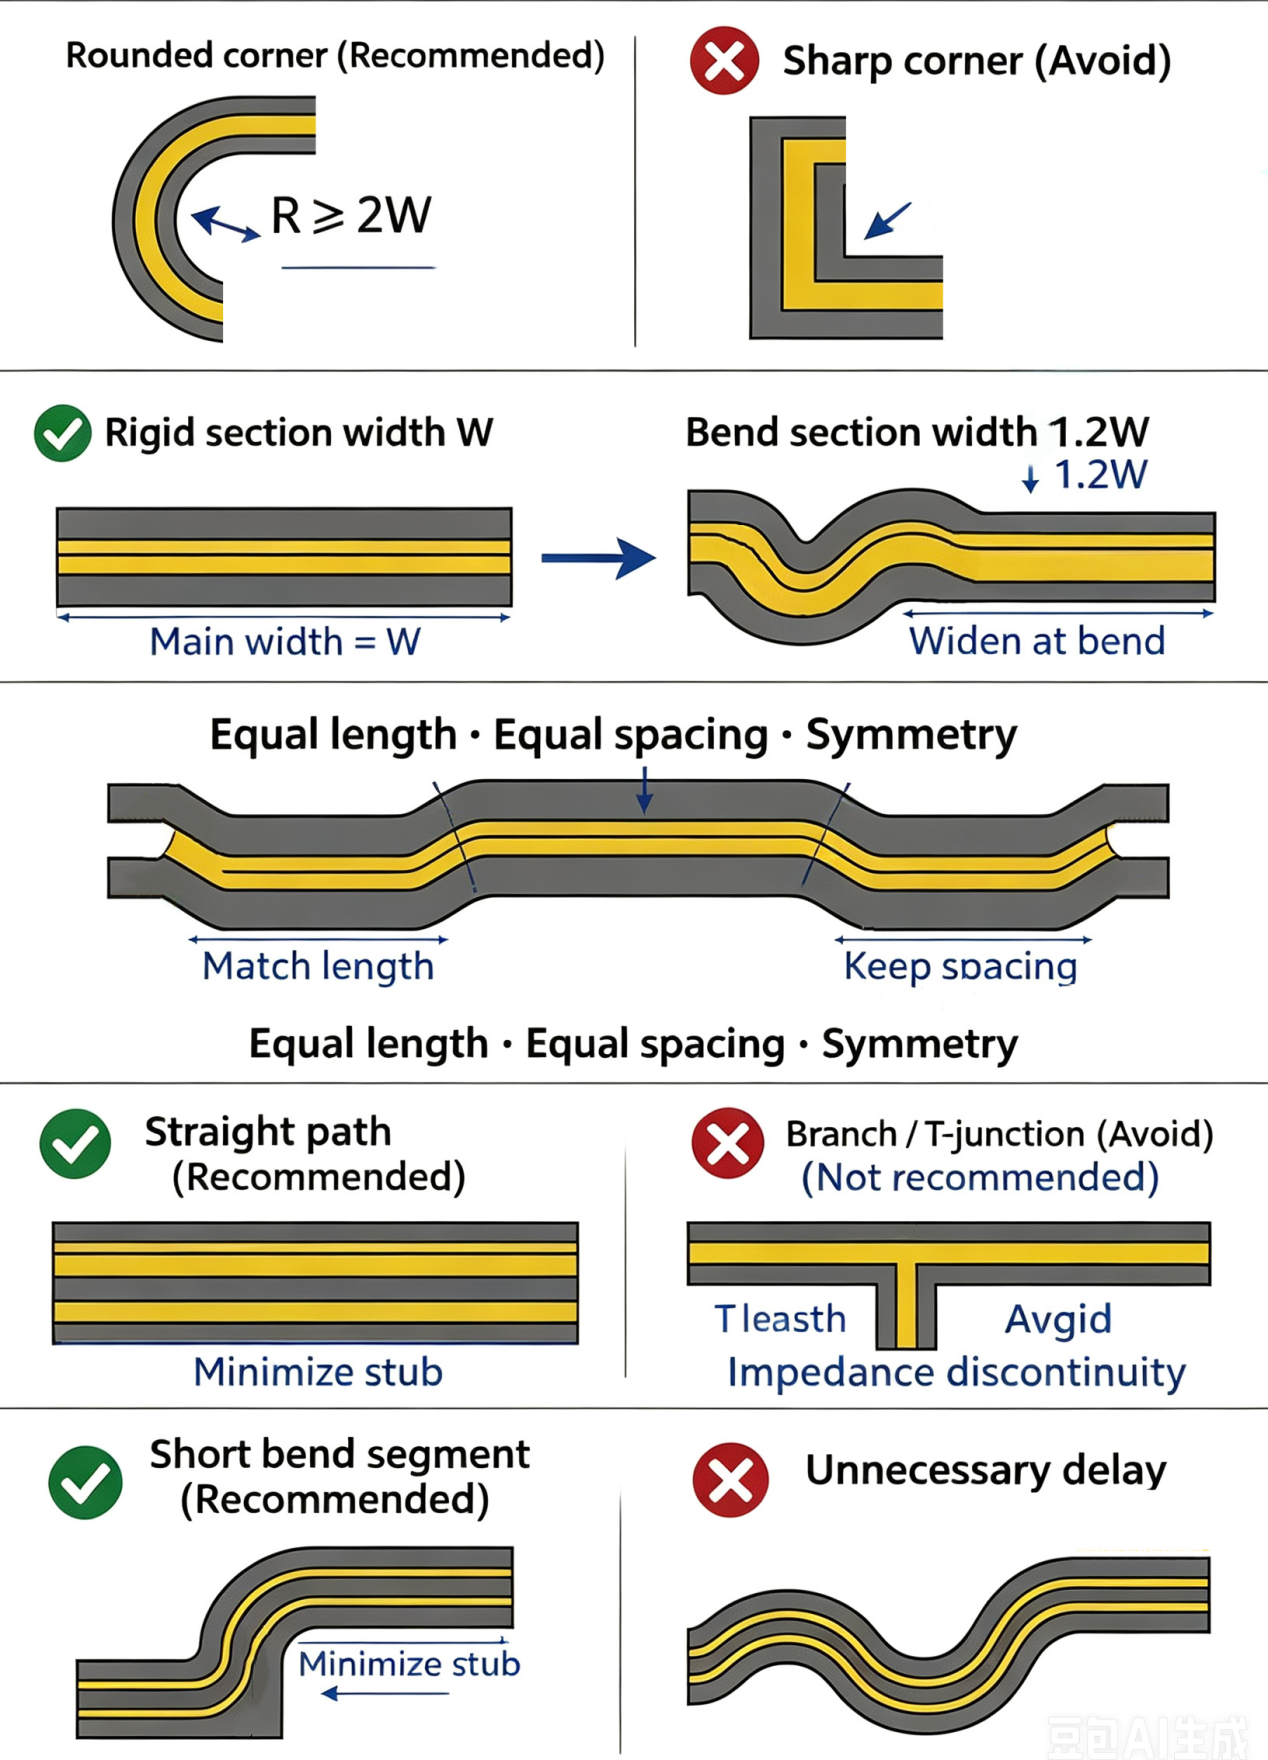
All routing corners inside the bending area should use smooth arcs instead of 90° or sharp angles. Sharp corners concentrate mechanical stress and significantly increase the likelihood of conductor failure. A corner radius of at least twice the trace width is recommended.
For traces subjected to repeated bending, increase the trace width by approximately 20–30% compared with traces in rigid sections. Wider traces improve tensile strength and enhance long-term flex reliability.
High-speed differential pairs should maintain constant spacing, equal lengths, and symmetrical routing throughout the flexible section. Uneven bending or inconsistent spacing can introduce impedance discontinuities, mode conversion, signal integrity degradation, and increased EMI.
Avoid T-junctions or branch traces inside flex regions. Branch points create localized stress concentration and are prone to fatigue cracking during repeated bending or vibration.
Minimize the total routing length within the flexible section. Excessive trace length increases bending fatigue and dielectric loss. Design the flex portion only as long as necessary to satisfy mechanical assembly requirements.
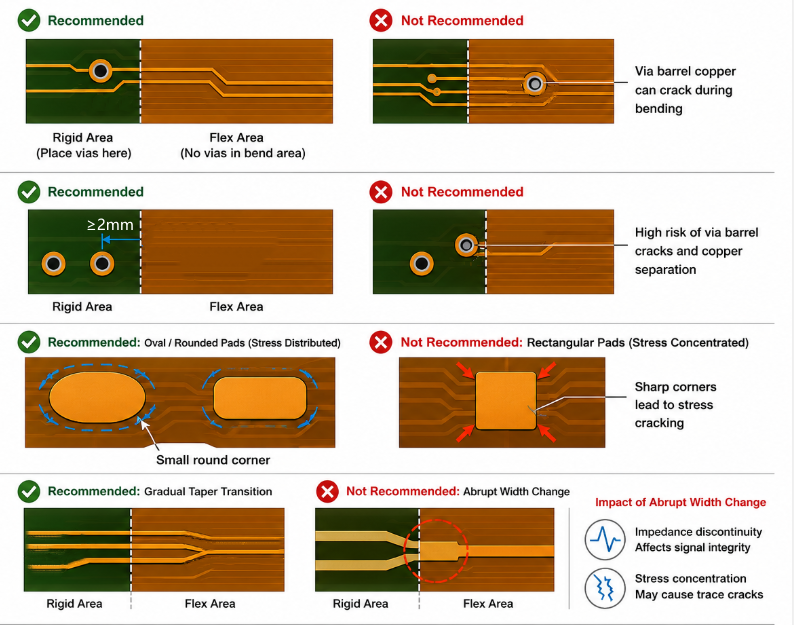
Keep plated through-holes (PTHs) to a minimum in flexible sections. Dynamic bend areas should never contain plated vias. If a layer transition is required, place the via in the rigid section instead. Copper inside via barrels is highly susceptible to cracking under repeated bending.
Vias located near the rigid-flex transition should be placed at least 2 mm away from the boundary. Since this area experiences the highest mechanical stress, vias placed too close can develop barrel cracks or copper separation over time.
Oval or elongated pads are preferred over standard rectangular pads in flexible areas because they distribute bending stress more evenly. Sharp pad corners should be rounded whenever possible to improve mechanical reliability.
When routing traces across the rigid-flex interface, gradually taper the trace width rather than changing it abruptly. Smooth transitions reduce both mechanical stress and impedance discontinuities.
For maximum reliability, COB pads and gold fingers should be placed in rigid sections. If they must be placed in flex areas additional stiffeners are required.
Do not use solid ground planes or large copper pours in dynamic flex regions. Continuous copper is prone to cracking during repeated bending. When grounding is required, cross-hatched (mesh) copper is recommended because it relieves mechanical stress while maintaining electrical continuity.
Complete ground planes should remain in rigid areas whenever possible. If EMI shielding is required in flexible sections, use thin copper shielding films or conductive adhesive films instead of thick copper planes.
Ground vias should be concentrated within the rigid section. Ground connections in the flexible section should be routed back to nearby rigid-area vias rather than placing dense via arrays inside bend regions.
Avoid placing analog/digital ground splits near the rigid-flex boundary. Mechanical deformation in this area can interrupt the return current path, increase crosstalk, and degrade overall signal integrity.
The dielectric constant (Dk) of polyimide (PI) differs significantly from that of FR4. Therefore, impedance calculations should be performed separately for rigid and flexible stackups. Do not apply the same trace width rules to both regions.
When high-speed differential pairs cross the rigid-flex boundary, allow sufficient routing margin because impedance changes slightly through the transition. Perform S-parameter simulations to minimize reflections and optimize routing.
Limit the routing length of high-speed signals within flexible sections. Excessive routing increases dielectric loss, insertion loss, and bending-related signal degradation. Keep the flex section only as long as required by the mechanical design.
Bending can slightly change the effective dielectric thickness, causing minor impedance shifts. Reserve adequate signal margin or equalization capability for critical high-speed interfaces.
The rigid-flex transition should feature smooth curved outlines instead of sharp inside or outside corners. Sharp corners are more likely to tear during routing, punching, or depanelization.
Apply PI stiffeners or stainless-steel stiffeners beneath component areas and connector pads. Stiffeners should terminate within the rigid section to improve soldering reliability and prevent deformation during assembly.
Flexible circuits naturally exhibit greater dimensional variation than rigid PCBs. A typical outline tolerance is ±0.15 mm for flexible sections, while rigid areas can generally achieve ±0.05 mm. Mechanical enclosures should include sufficient clearance for flex movement.
The bend radius should satisfy the application requirements:
Smaller bend radii dramatically increase the risk of copper cracking and substrate failure.
Edge connectors should always be reinforced with stiffeners. Gold fingers should not be placed directly on unsupported flexible material, as repeated insertion and removal can cause deformation, pad lifting, or plating wear.
Flexible sections should use high-elongation flexible solder mask instead of conventional rigid PCB solder mask. Standard solder mask is relatively brittle and can crack or peel off during repeated bending, leaving copper traces exposed and unprotected.
Avoid large solder mask openings in bending regions whenever possible. Exposed copper is more susceptible to oxidation and mechanical wear during flexing. Unless electrical exposure is required, copper traces should remain protected by the solder mask.
Electroless Nickel Immersion Gold (ENIG) is generally the preferred surface finish for rigid-flex PCBs due to its excellent solderability and corrosion resistance. Thick electroplated hard gold is not recommended for dynamic flex sections because its relatively brittle plating can crack after repeated bending.
Silkscreen markings should not cross the bend centerline. The cured ink increases the local thickness and stiffness of the flex area, creating stress concentration points that may initiate cracking during repeated bending.
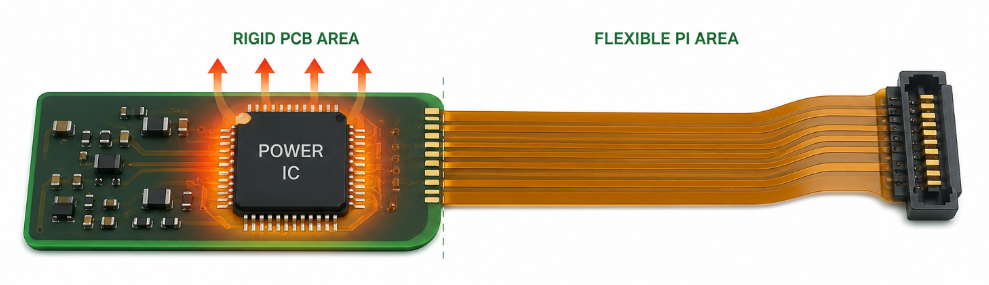
Power ICs, processors, and other high-power components should always be located in the rigid section. Polyimide has significantly lower thermal conductivity than FR4, making the flexible area unsuitable for efficient heat dissipation. Prolonged exposure to elevated temperatures also accelerates material aging.
Thermal copper pours, thermal vias, and heat-spreading structures should remain within the rigid region. Extending these features into flexible sections increases stress caused by the different thermal expansion rates of FR4 and PI, especially during thermal cycling.
Avoid routing flexible sections close to transformers, power inductors, MOSFETs, or other high-temperature components. Continuous thermal exposure reduces the fatigue life of the flexible substrate and shortens its bending cycle life.
Compared with rigid PCBs, flexible circuits generally require more conservative design rules. A common manufacturing capability is 4 mil/4 mil (trace width/spacing) or larger. Designs with finer features should be verified with the PCB manufacturer in advance to ensure reliable fabrication.
Rigid-flex panels should include process rails, handling frames, and breakaway tabs to support fabrication and assembly. Never use the flexible section as the gripping or conveyor area during manufacturing.
The lamination process must carefully control temperature, pressure, and curing conditions because FR4 and PI materials respond differently during lamination. Improper process parameters may lead to voids, delamination, or damage to the flexible circuitry.
Laser cutting is the preferred depanelization method for rigid-flex PCBs. Avoid V-scoring or mechanical punching across the rigid-flex interface, as these methods introduce excessive mechanical stress and may tear the flexible substrate.
During panelization and assembly, the flexible bending area should remain suspended with adequate clearance underneath. Production fixtures and assembly tooling should never press directly against the flex region, preventing damage to copper traces and the substrate.
For products operating in vibration-prone environments, allow appropriate routing flexibility and mechanical margin in the bending section. This helps reduce copper fatigue and improves long-term reliability.
The difference in the coefficient of thermal expansion (CTE) between FR4 and PI creates mechanical stress during temperature cycling. Avoid placing dense routing, vias, or critical structures directly along the rigid-flex transition. Leave sufficient space to accommodate thermal expansion.
For outdoor, industrial, or high-humidity applications, additional PI protective films or laminated protective layers can help prevent moisture ingress, copper oxidation, and corrosion, extending product reliability.
Products designed for dynamic bending should undergo bend-life simulation and reliability testing during development. Typical consumer electronics are often designed for 10,000 or more bending cycles, while industrial and automotive applications may require 100,000 cycles or higher depending on the operating environment.
When designing a rigid-flex PCB layout, avoiding common mistakes is just as important as following best practices. The following issues are among the most frequent causes of mechanical failure and reliability problems:
Designing a reliable rigid-flex PCB layout requires balancing electrical performance, mechanical durability, and manufacturability. From selecting the right materials and optimizing the PCB stackup to controlling bend radius, routing, impedance, and DFM, every design decision directly impacts long-term product reliability and manufacturing yield.
If your project involves complex rigid-flex PCB design, high-speed routing, or challenging mechanical constraints, PCBWay Design Service can help optimize your PCB layout from the early design stage. Combined with PCB fabrication and assembly services, PCBWay provides a complete solution to help bring your rigid-flex PCB from concept to production with greater confidence and efficiency.