Electrical discharge machining, also widely known as spark erosion, spark machining, or electro-erosion machining, is a non-traditional manufacturing process. By utilizing controlled pulse discharges between an electrode and a conductive workpiece, it generates localized extreme temperatures to remove material via electro-erosion. Today, electrical discharge machining has become an indispensable core technology in precision mold making, aerospace components, and medical device manufacturing.
The fundamental principle of electrical discharge machining relies on thermal energy produced by high-frequency electric sparks to locally melt and vaporize material. During processing, a micro-gap is consistently maintained between the electrode and the conductive workpiece, where dielectric fluid flows to provide electrical insulation and continuous chip flushing.
Different non-traditional machining processes utilize specific dielectric media based on cooling and accuracy requirements:
Material removal follows a dynamic, highly controlled micro-erosion cycle:
Workpiece hardness presents minimal limitation to processing feasibility; however, electrical conductivity and thermophysical properties directly influence overall removal rate and final surface quality.
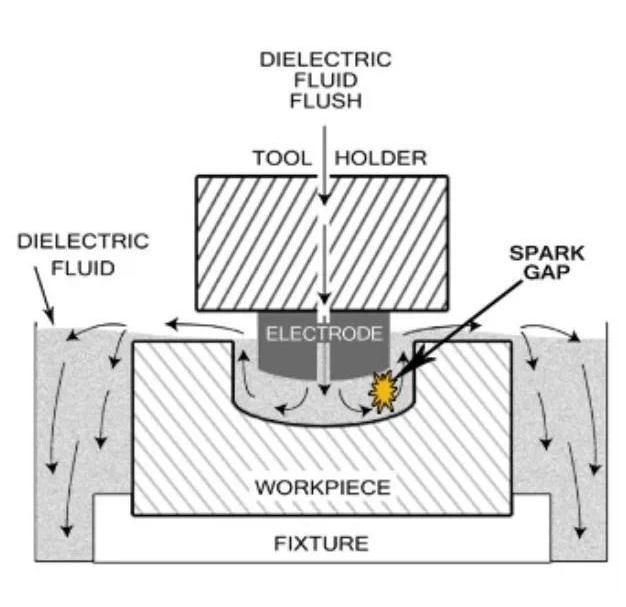
(EDM Working Principle)
Based on kinematics, electrode configuration, and target industrial applications, non-traditional electro-discharge manufacturing is categorized into four primary configurations:
In a standard Wire EDM setup, a continuously traveling thin brass or coated wire (typically 0.1–0.3 mm in diameter) serves as the cutting electrode tool. Guided by computerized numerical control, high-precision trajectory planning and continuous wire feeding ensure high processing stability. Under optimal machine calibration, material selection, and parameters, modern cnc wire cut technology can easily achieve sub-micron dimensional control. Parts processed via cnc wire cut exhibit virtually no mechanical burrs common in conventional milling, although minor spark erosion tracks and a thin recast layer remain. This process is extensively applied to complex 2D profiles, narrow slots, irregular keyways, and tapered precision geometries.
Sinker EDM utilizes custom-machined 3D copper or graphite electrodes. Controlled spark erosion between the shaped electrode and workpiece gradually replicates the exact inverted form onto the part. This method excels at forming blind cavities and intricate concave structures. Because electrode wear occurs dynamically during operation, precise multi-stage tool switching is essential. Sinker units often incorporate advanced cnc edm controllers to compensate for wear paths, serving as a pillar process in injection mold, die casting, and stamping tool production.
Hole drilling EDM uses a tubular rotating electrode combined with internal high-pressure dielectric flushing to clear erosion debris. It specializes in drilling tiny deep holes or angled channels into hard metals such as cemented carbide and nickel superalloys. Widely used for turbine blade cooling holes and fuel nozzle micro-apertures, it eliminates traditional drill bit breakage issues. Additionally, high-speed hole drillers are regularly deployed to produce starting pilot holes for subsequent cnc wire edm cutting operations.
Micro EDM utilizes ultra-fine electrodes and extremely small pulse discharge energy to produce micro-scale features down to a few micrometers. By minimizing single-discharge energy, the thermal affect zone (HAZ) is significantly reduced, making it ideal for medical implants, micro-fluidic channels, and micro-electronic components.
Manufacturing Note: While electro-discharge processing solves difficult geometry problems, design engineers must account for material conductivity limits, lower volumetric removal rates, and thermal surface alterations.
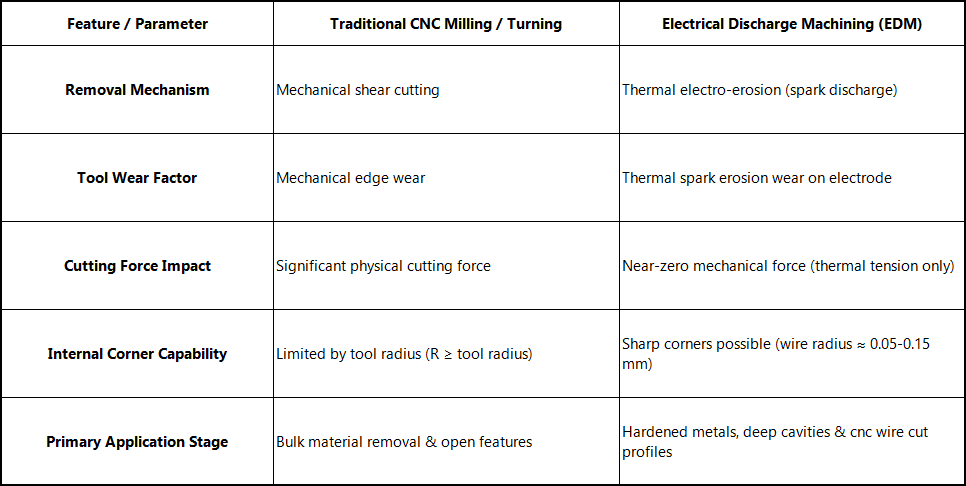
Traditional CNC milling relies on solid cutting tools to mechanically shear metal chips. Mechanical tool wear is present, internal sharp corners are limited by tool radii, and thin-walled parts risk mechanical deflection. In contrast, cnc edm relies on thermal spark erosion without physical cutter contact pressure. In modern toolrooms, these technologies are complementary rather than competing: heavy material removal and outer profiles are first handled by high-efficiency CNC milling, after which precision features are finished using a high-precision cnc wire edm unit or sinker machine.
Electrical discharge techniques focus on high-precision, high-value manufacturing sectors:
Rather than replacing traditional CNC machining, electrical discharge machining serves as a crucial technical complement for hard metals, complex cavities, deep slots, and micro-scale features. Its low mechanical force and exceptional hard-material capability deliver immense value across aerospace, mold making, and medical industries. Combining conventional CNC roughing with final electro-discharge finishing remains the industry standard for achieving optimized cycle times, tight tolerances, and superior part quality.